ZQ-1.0 Industrial Steam Engineering System
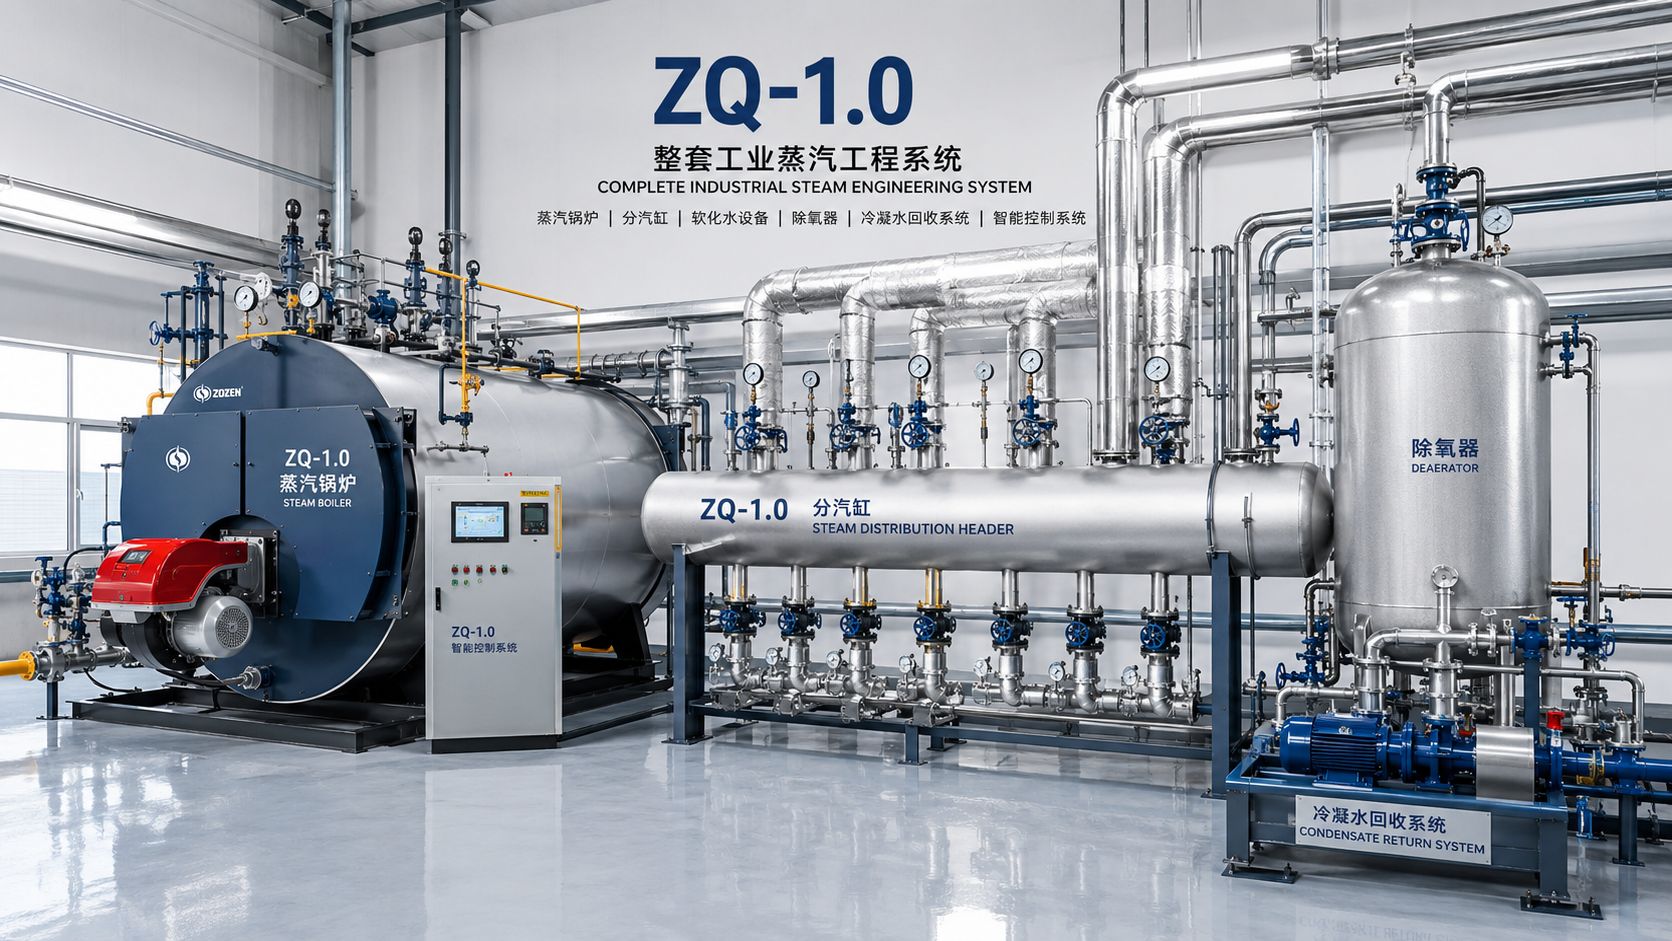
Rated evaporation capacity 1.0t/h, with full set of accessories including steam distribution and condensate recovery
产品特性
产品描述
ZQ-1.0 Industrial Steam Engineering System
The ZQ-1.0 Industrial Steam Engineering System is a complete industrial steam supply solution with a rated evaporation capacity of 1.0t/h, comprising five main modules: steam generator main unit, steam distribution piping network, condensate recovery system, water treatment system, and automatic control system. Turnkey delivery—users can start production simply by connecting water and power.
What is Steam Engineering
Steam engineering is a systematic engineering discipline that uses steam as a heat carrier to provide thermal energy for industrial production processes. It does not merely supply a single boiler, but represents a comprehensive solution covering the entire process of steam generation, transmission, usage, condensate recovery, water treatment, and automatic control.
- Steam Generation System: Steam boiler or steam generator that heats water into saturated steam meeting process requirements.
- Steam Transmission System: Steam piping, steam headers, pressure reducing valves, steam traps, etc., delivering steam safely and efficiently to each steam consumption point.
- Water Treatment System: Water softening and deaeration equipment to ensure boiler feedwater quality meets standards, reducing scaling and corrosion.
- Condensate Recovery System: Recovers thermal energy and water resources from condensate, reducing fuel and water treatment costs.
- Automatic Control System: Enables automatic regulation and remote monitoring of key parameters such as pressure, temperature, flow rate, and water level.
System Advantages
Turnkey Delivery: From scheme design, equipment selection, installation and commissioning to operation and maintenance, Jingyu Thermal Energy provides full-process engineering services, suitable for steam-consuming enterprises in food, chemical, pharmaceutical, and laundry industries.
Condensate Recovery: Equipped with a high-efficiency condensate recovery system capable of recovering most of the steam condensate. Condensate temperature is typically around 80-95°C, and recovery significantly reduces fuel and water treatment costs.
Intelligent Management: Adopts a PLC + touch screen control system that monitors key parameters such as steam pressure, temperature, flow rate, and water level in real time, supporting fault alarms, automatic water replenishment, automatic blowdown, and automatic pressure regulation.
Typical Applications in Northeast China
Suitable for food processing, pharmaceutical, chemical, laundry, and heating support projects in Northeast China regions such as Harbin, Changchun, and Shenyang. Designed specifically for severe cold regions, the system emphasizes pipeline insulation, freeze protection, condensate recovery, and stable winter operation.
Technical Parameters
| Parameter | Specification |
| Rated Evaporation Capacity | 1.0t/h |
| Rated Steam Pressure | 1.0MPa |
| Steam Temperature | Approx. 184°C (Saturated) |
| Design Thermal Efficiency | ≥95% |
| Fuel Type | Natural Gas / Biomass / Electric (Optional) |
| Condensate Recovery Rate | ≥90% |
| Control Method | PLC Automatic Control + Remote Monitoring |
| Supporting Services | Design + Installation + Commissioning + Training + O&M |
Product Features
- Condensate recovery for energy saving and consumption reduction
- Automatic blowdown reduces manual intervention
- Stable steam quality adaptable to various production processes
- Complete accessories facilitate implementation of new and retrofit projects
服务热线
18686730186